
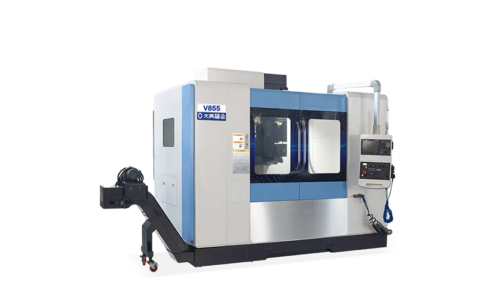
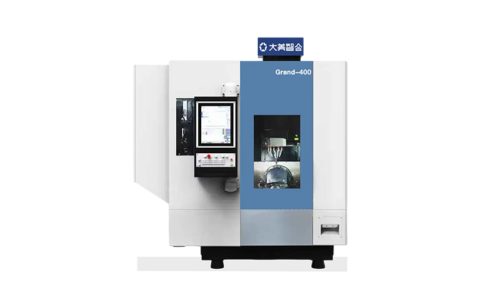
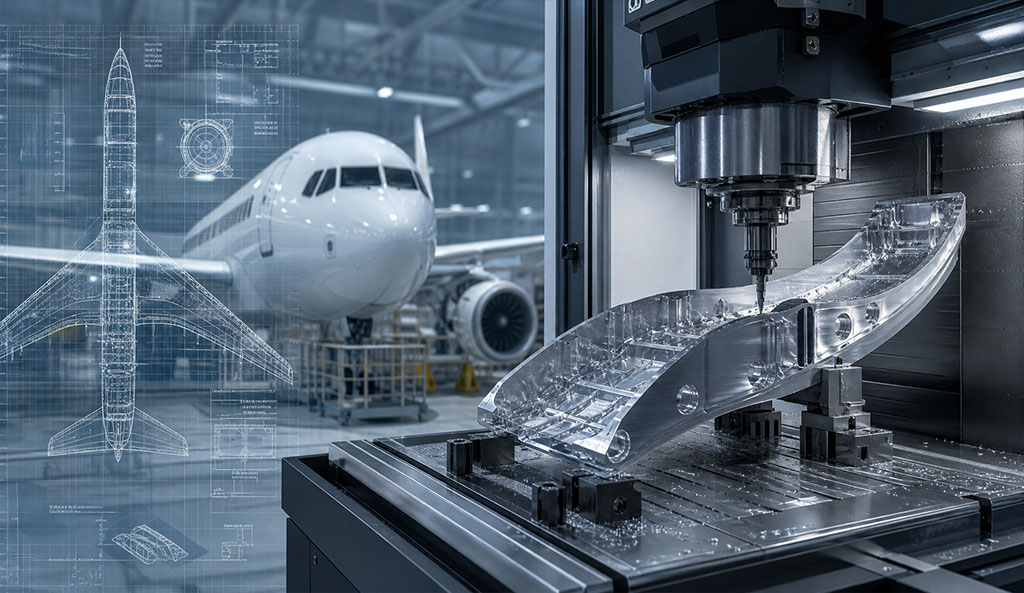
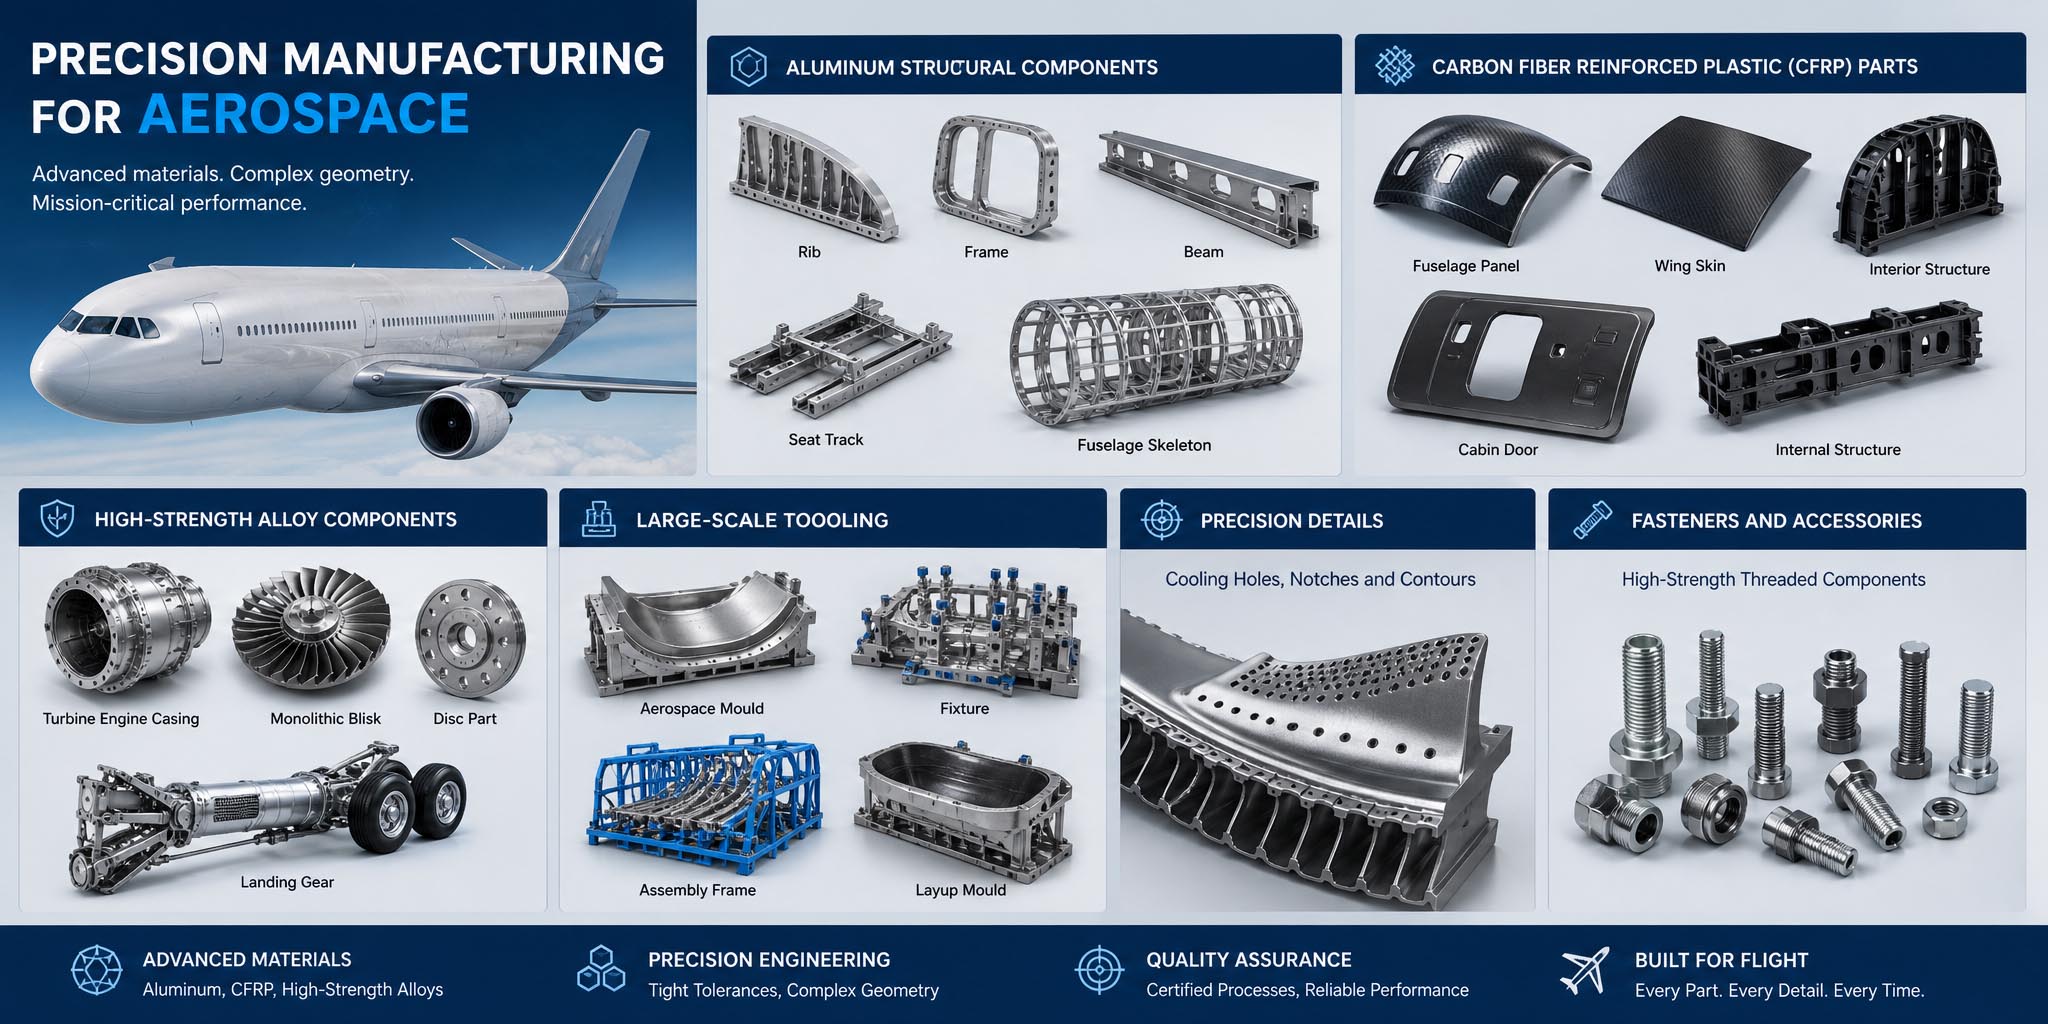
Aerospace manufacturing demands exceptional precision, uncompromising safety, and strict regulatory compliance. Every component must withstand extreme operating conditions. Grand CNC draws on decades of precision machining experience to deliver high-performance CNC solutions for OEMs and tier suppliers, providing reliable technology that meets the industry’s most rigorous standards.
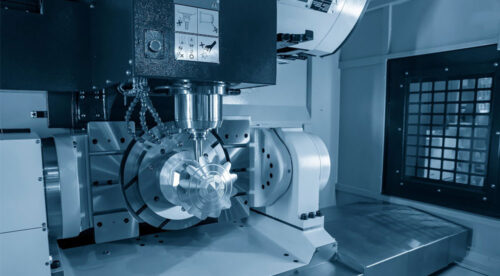
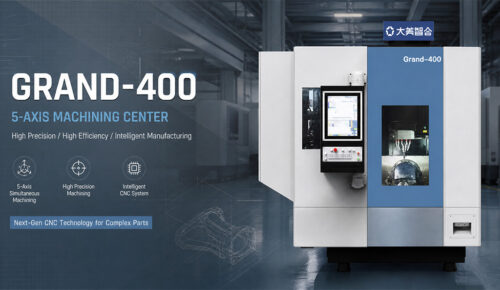
Complex aerospace parts—wing spars, bulkheads, panels, engine casings—require multi-axis platforms with large work envelopes. Grand CNC's advanced 5-axis solutions machine oversized aerospace structures with rigidity and accuracy for high-tolerance aluminum and high-temperature alloys. Our proprietary structural designs optimize cutting force transmission for stable heavy titanium/Inconel removal and high-speed aluminum/composite machining.
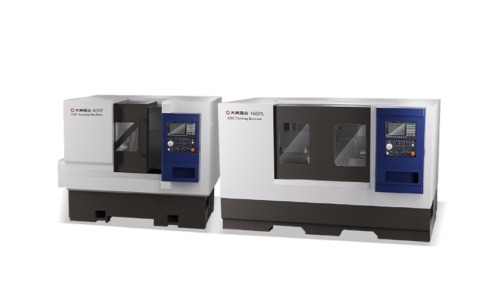
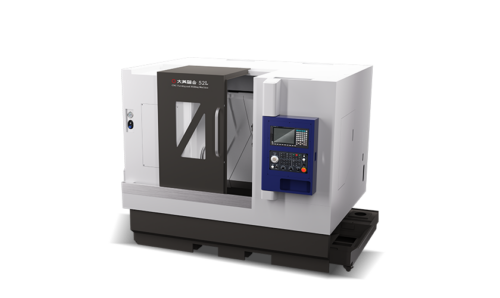
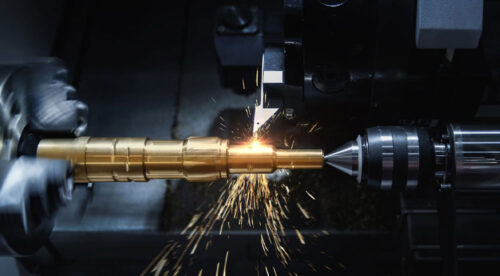
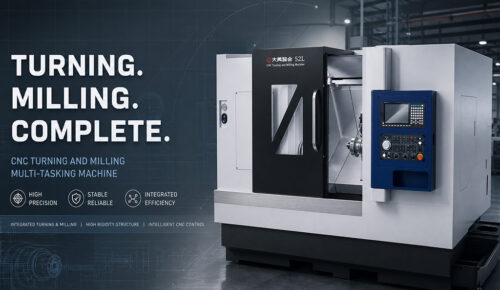
Large rotating aerospace components – turbine casings, landing gear parts, engine housings, and bearing races – naturally suit vertical turning lathes (VTLs). Grand CNC provides VTL solutions that handle workpieces with swing diameters exceeding 40 inches. We combine heavy‑duty turning capacity with optional live tooling, C‑axis, and Y‑axis, enabling complete machining in a single setup. This approach reduces setup time, improves concentricity, and eliminates cumulative errors from multiple operations.
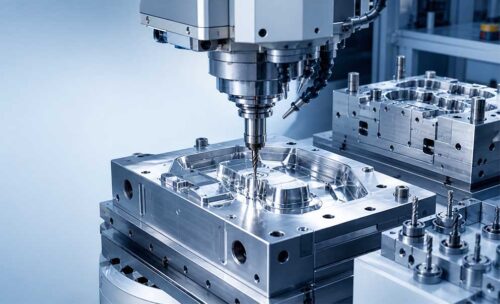
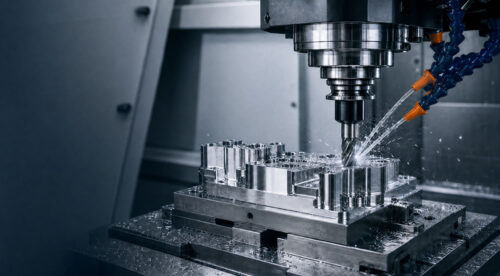
Grand CNC supplies double-column bridge mills with exceptional rigidity and versatility for large aerospace fixtures, dies, molds, and structural parts. One-piece Meehanite cast-iron columns and box-way construction resist heavy-roughing deflection while maintaining precision for tooling and secondary operations. Whether machining large mold bases, layup tooling, or assembly fixtures, our bridge mills deliver aerospace-grade stability and accuracy.
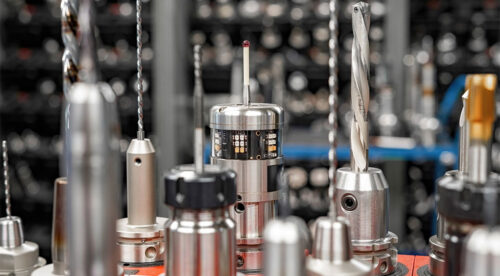
Aerospace components frequently feature hole geometries that conventional drilling cannot achieve. Turbine cooling holes, hydraulic manifolds, landing gear shafts,fuel systems demand extreme depth-to-diameter ratios, straightness, and finish in hard-to-cut superalloys.
Grand CNC's high-precision gun drilling systems maintain hole straightness, bore tolerance, and surface quality at depth-to-diameter ratios up to 200:1. Whether drilling turbine cooling channels or landing gear oil passages, our gun drilling solutions are purpose-built for your application.
Furthermore, Small-hole EDM drilling ideal for 0.010–0.040″ compound-angle cooling holes in turbine blades, vanes, combustion liners through nickel superalloys. This process erodes material electrically, eliminating hardness obstacles and tool deflection concerns. Turbine blades need 30–80 cooling holes; our multi-axis EDM with ATC drills them lights-out from one program.
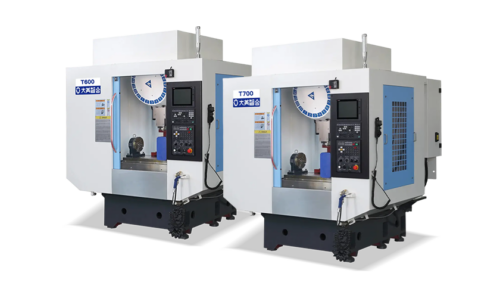
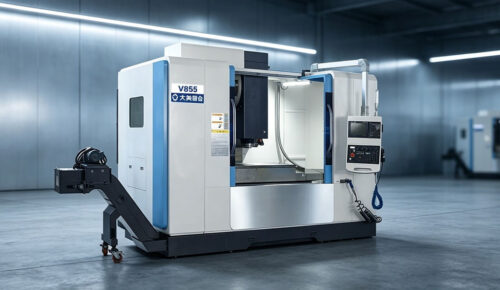
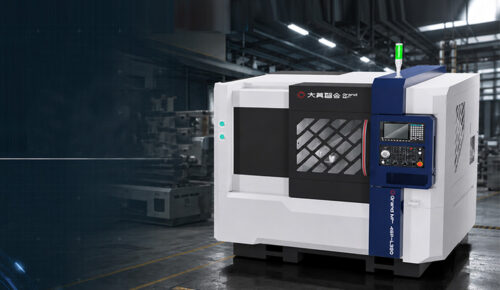
Horizontal machining centers (HMCs) are a natural fit for aerospace structural parts. The horizontal spindle orientation allows chips to fall away from the cutting zone under gravity. Pallet changers cut setup time; multi-side access completes complex brackets, housings, and frames in fewer operations. Grand CNC offers HMC solutions engineered specifically for aerospace workloads – ranging from high‑speed contouring of medium‑sized aluminum and light‑alloy components to heavy‑duty machining of large superalloy parts with spindle torque exceeding 500 Nm and workpiece capacities up to several tons. Both configurations can integrate with pallet pools and linear pallet systems for unattended production.
Our HMC platforms handle large-format, 10,000-lb workpieces with flexible automation, delivering Japanese-grade precision and thermal stability for high-mix aerospace.
Feel free to contact us for more information.
Aerospace shops typically run a mix of platforms because no single machine handles every part family well. A modern aerospace facility usually pairs a 5‑axis CNC for complex contoured parts (impellers, structural brackets, ribs) with horizontal machining centers for high‑volume engine casework on pallets, plus a vertical mill or large bridge mill for tooling and oversized structures. Round components such as turbine casings, bearing housings, and landing gear cylinders move to vertical turning lathes or large turning centers, while EDM hole drilling handles cooling holes in hot‑section parts and gun drilling produces hydraulic actuator bores. The right portfolio ultimately depends on the mix of airframe, engine, and accessory work that the shop targets.
Four materials mainly drive equipment‑selection discussions. Titanium alloys (Ti‑6Al‑4V is the workhorse) and nickel‑based superalloys (Inconel 718, Waspaloy, Rene) demand high spindle torque, generous through‑spindle coolant, and rigid box‑way construction. Aerospace‑grade aluminum, in contrast, requires very high spindle RPM (often 20,000 and above), aggressive chip clearance, and dynamic stiffness against chatter. CFRP composites present a separate challenge entirely – abrasive dust degrades unsealed machines, and dimensional drift originates from temperature rather than cutting forces, so dedicated platforms with integrated dust extraction and thermally stable structures become essential.
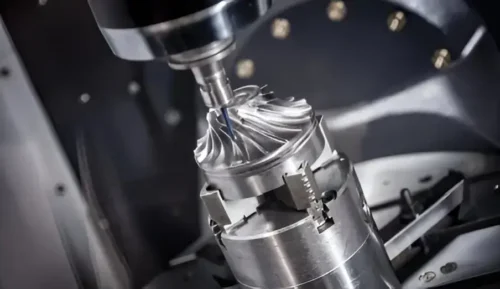
Modern airframe and engine parts incorporate undercuts, compound curvatures, and reference surfaces on faces that a 3‑axis spindle cannot reach without re‑clamping. Every additional setup on a complex titanium fitting can introduce 0.0005″ to 0.002″ of position error that accumulates across operations – and on a high‑value forging, that error budget quickly evaporates. Holding the part once and tilting either the spindle or the workpiece eliminates that stack‑up. Economic pressures drive major OEMs to move structural part-making onto purpose-built 5-axis platforms rather than chaining setups across machines.
The crossover point arrives when shops reach production volumes of small-to-medium aerospace parts: brackets, gearbox housings, actuator bodies, accessories. On an HMC, chips fall away from the cutter under gravity instead of recutting in the pocket, which substantially extends tool life on titanium and superalloys and improves bore finish on deep features. Tombstone fixtures hold four to eight parts per face; one operator tends pallets; pallet-pool automation extends utilization into unattended shifts. Vertical machining centers still win for prototyping, very low‑volume work, and large fixtures that will not fit on a pallet – but for repeat aerospace production, HMC economics typically pay back the price premium within 18 to 24 months.
Once a part exceeds roughly 80 inches in any direction – wing spars, fuselage frames, large mold bases, layup tooling, assembly fixtures – bridge mills and gantry‑style 5‑axis machines become the only practical options. For heavy steel and titanium tooling work, bridge mills with sliding‑column series carry large tables with one‑piece cast‑iron columns that resist deflection under heavy roughing. For high‑MRR aluminum airframe machining, gantry 5‑axis platforms are designed differently – engineered to keep cutting forces flowing through the structure rather than transferring vibration into the foundation. The practical decision usually breaks on chip volume: gantries for high‑speed aluminum, bridge mills for heavy alloy tooling and dies.
AS9100 (aerospace's adaptation of ISO 9001) forms the foundational quality system, but two other certifications carry equal weight: Nadcap accreditation for special processes (heat treat, NDT, EDM, surface treatments) and customer‑specific approvals from OEMs such as Boeing, Airbus, Rolls‑Royce, Pratt & Whitney, and Bombardier. Machines themselves do not carry these certifications – the shop does – but the equipment must support the full documentation chain. This means in‑process probing routines, controllers that capture spindle load and override events for traceability, thermal stability that holds tolerance across an 8‑hour run rather than drifting after part 50, and machine monitoring software increasingly required by OEM auditors to prove uptime and process consistency.
A well‑specified machine running aerospace duty cycles typically delivers 15 to 25 years of production service – often longer if the casting and spindle are matched to the work. The biggest determinants include structural design (Meehanite cast iron with box ways outlasts welded weldments and linear rails on heavy titanium cuts), spindle selection (gear‑driven heads for low‑RPM high‑torque alloy work; direct‑drive for high‑RPM aluminum), thermal management, and how disciplined the shop remains about coolant chemistry.
We recommend running five practical filters before any quote arrives: (1) does the work envelope cover your largest planned part with fixturing and tool clearance, (2) does the spindle's torque‑and‑RPM curve actually match your dominant material under cutting load, (3) can the machine integrate with the pallet and robotic automation you will add later (not just what you can afford this year), (4) what are the realistic accuracy and thermal stability numbers under production conditions versus the brochure spec, and (5) what does the parts and field service infrastructure look like in your region. The last filter is the one most aerospace buyers underweight until the first time they need a critical spare part on a Friday night.
From solution selection to mass production, we provide machine tools and full-lifecycle support to boost efficiency, quality, and competitiveness. Contact us anytime to learn more about our CNC machine tools.
 Industry
 Products
 Products
 Products
 Products
 Products

English

French

Portuguese

Spanish